
In food processing, timing matters. When a critical piece of equipment needs replacing, production can't always wait months for a new unit to arrive. Orders still need to go out, customers still expect deliveries, and your team still has a plant to run.
Sometimes, the challenge isn't finding the right long-term solution. It's figuring out how to keep things moving until that solution is ready.
For food and beverage manufacturers, equipment such as flavorizers, vacuumizers, deaerators, and food additive systems can play an important role in product quality and process consistency. When one of these units needs replacing, upgrading, or adding to an existing line, exploring the used equipment market may offer another path forward.
That's where Genemco comes in.
What Are Industrial Flavorizers, Vacuumizers, and Deaerators?
Although these machines can be used in related food processing environments, each serves a different purpose. Understanding their roles can help you identify the equipment that best fits your operation.
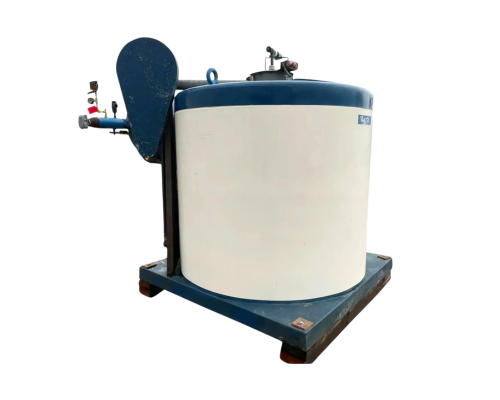
Industrial Flavorizers
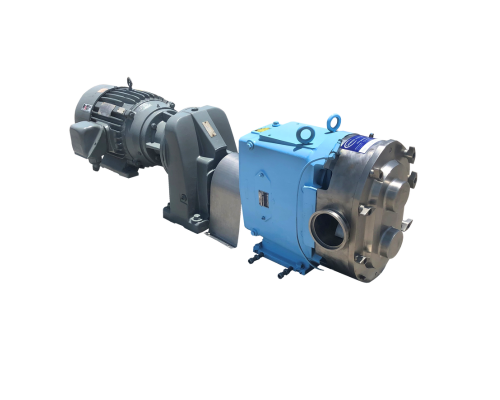
Industrial flavorizers are used in food processing applications involving flavor development, flavor incorporation, or the handling of flavor-related ingredients. Depending on the machine's design and intended process, a flavorizer may support a specific stage of product preparation or treatment.
These units can be relevant to manufacturers working with food ingredients, dairy products, beverages, sauces, and other formulated foods. The exact function depends on the equipment design, so confirming the original application and specifications is important when sourcing a replacement.
Image from Genemco
Link to Flavorizers, Vacuumizers, Deaerators & Food Additive Skids
Industrial Vacuumizers
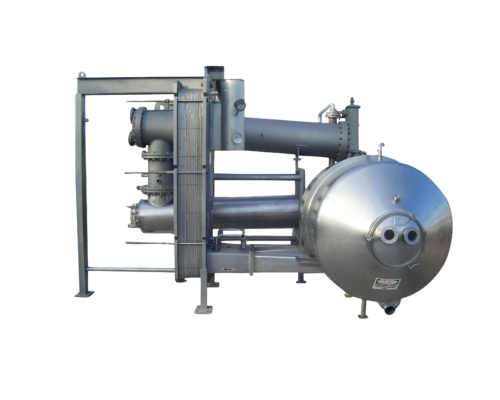
Vacuumizers use reduced pressure to support processing operations. Depending on the system, vacuum processing may help remove entrained air or gases, manage volatile components, or support thermal processing under controlled conditions.
In food manufacturing, vacuum technology can be useful when processors need greater control over product characteristics, processing conditions, or downstream operations.
For example, Genemco's listed DeLaval Vacuumizer is identified as a separator for an HTST system, with a stated capacity of 35,000 pounds per hour. That makes reviewing the actual equipment specifications especially important when evaluating a potential replacement or addition to an existing line.
Image from Genemco
Link to Flavorizers, Vacuumizers, Deaerators & Food Additive Skids
Industrial Deaerators
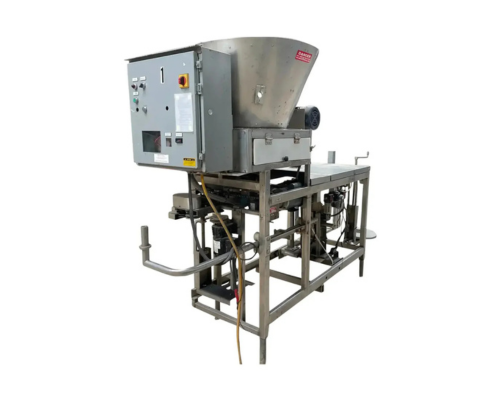
Deaerators are designed to remove entrained or dissolved gases from a liquid or product stream. In food processing, removing unwanted air can help address concerns related to oxidation, foaming, product consistency, and downstream processing performance, depending on the application.
Deaeration may be relevant in dairy processing, beverage production, liquid food manufacturing, and other applications where air in the product can create challenges.
The specific results depend on the product, equipment design, and operating conditions.
Image from Genemco
Link to Flavorizers, Vacuumizers, Deaerators & Food Additive Skids
Food Additive Skids and Related Process Equipment
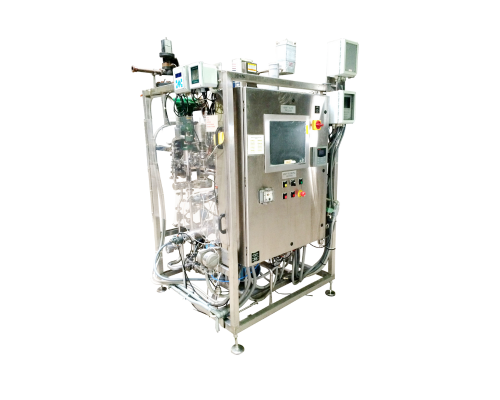
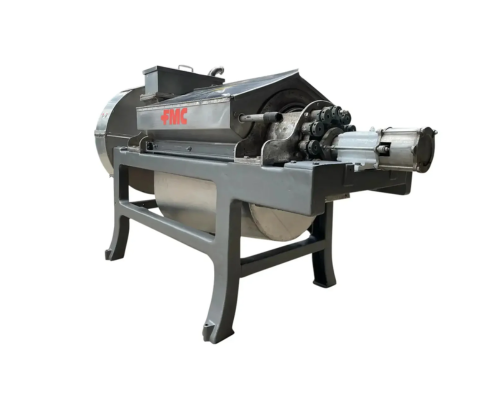
Not every processing challenge calls for a large standalone vessel. Food additive skids and related systems can support the handling and introduction of ingredients into a manufacturing process.
A properly selected system can help a facility manage a particular production step while maintaining consistency and meeting the requirements of the overall process.
The key is finding equipment that fits the application—not simply choosing a unit because its name sounds familiar.
Image from Genemco
Link to Flavorizers, Vacuumizers, Deaerators & Food Additive Skids
Which Industries Use This Type of Equipment?
Flavorizers, vacuumizers, deaerators, and additive handling equipment can be relevant across several segments of the food processing industry.
Dairy processing: Milk, cream, whey ingredients, and other dairy products may require specialized processing equipment for separation, deaeration, thermal treatment, or ingredient handling.
Beverage manufacturing: Juice, beverage bases, concentrates, syrups, and other liquid products may benefit from appropriate vacuum or deaeration processes, depending on the formulation and production method.
Food ingredient manufacturing: Ingredient producers often need equipment that supports consistent preparation and handling of specialized ingredients used by other manufacturers.
Sauces, dressings, and condiments: Liquid and semi-liquid food products may require controlled processing, ingredient addition, or air removal to achieve desired product characteristics.
Prepared foods and other packaged products: Depending on the recipe and process, specialized vessels and processing systems can support product preparation and help maintain consistent production.
These are potential application areas, not a guarantee that every type of flavorizer or vacuumizer is suitable for every product. Process requirements, sanitation standards, materials of construction, operating pressures, and temperatures all need to be considered before equipment is selected.
Why Consider Used Food Processing Equipment?
When a production line is waiting on a piece of equipment, the usual options may feel limited: wait for a new unit, redesign the process, or try to make the existing equipment last a little longer.
But there may be another option.
A suitable used unit can sometimes help fill the gap, whether you are replacing equipment that has failed, expanding production capacity, or keeping a project on schedule while a new system is being manufactured.
Here are a few reasons food processors explore used equipment:
-
Potentially shorter procurement timelines: An existing unit may be available sooner than a newly manufactured system, although inspection, preparation, shipping, and installation still take time.
-
A different approach to capital spending: Used equipment may offer a lower initial purchase cost than new equipment, depending on the unit and its condition.
-
Support for temporary production needs: A compatible unit may help bridge a gap while a permanent solution is being completed.
-
More options for older systems: When a machine is difficult to replace with an identical new model, the used equipment market may provide additional possibilities to investigate.
-
Flexibility for planned projects: An existing unit may be worth exploring when you need to maintain production during an upgrade or expansion.
Of course, used equipment isn't automatically the right choice. Compatibility, condition, documentation, cleaning requirements, installation costs, and any necessary modifications must be evaluated. The goal is to find a practical solution that meets the needs of the application.
Why Choose Genemco?
At Genemco, we understand that equipment purchasing isn't always a straightforward process. Sometimes you're planning an upgrade months in advance. Other times, you're working against a deadline and need to explore every reasonable option.
Our used industrial food processing and refrigeration equipment inventory gives businesses another resource when searching for specialized machinery.
Whether you're looking for a flavorizer, vacuumizer, deaerator, or related process equipment, Genemco can help you explore available units and determine whether one may be a fit for your requirements.
Explore Equipment That May Fit Your Application
Genemco's inventory includes several examples of the equipment categories discussed here:
-
Cherry Burrell Flavorizer — Stainless Steel: A specialized flavor-processing unit worth exploring for applications that match its intended duty.
-
DeLaval Vacuumizer — Stainless Steel: A Model 650 vacuumizer listed for an HTST system, with a stated capacity of 35,000 lb/hr.
-
Crepaco Deaerator Tank: An option to investigate for compatible deaeration applications.
-
Vacu-Therm — 50 Gallon: A 50-gallon unit to consider when evaluating vacuum-related processing requirements.
-
Food Additive Skid — 12 Gallons: A smaller-capacity option to explore for suitable ingredient-handling applications.
Equipment availability can change, and specifications should always be confirmed against the needs of your process. These listings are a starting point for the conversation—not a substitute for an engineering review.
OEMs: We Want to Help You Be the Hero
If you're an original equipment manufacturer (OEM), you know that selling a piece of equipment is only part of the job. You're also building a relationship, solving a customer's problem, and delivering a system designed to serve them for years to come.
But what happens when your customer needs equipment now, and your new unit has a long manufacturing lead time?
Your customer may be facing a production bottleneck. A replacement may be urgent. And while your team is working hard to deliver the right long-term solution, the customer still needs to keep the plant running.
We don't want to take the sale from you. We want to help you make the sale—and make you the hero.
Think of Genemco as another resource in your toolbox. If a suitable used unit is available and compatible with the application, it may help your customer bridge the gap while your new equipment is being manufactured.
In some situations, that interim unit can be like a bandage. In a more critical situation, it may be the tourniquet that helps keep an operation going until the permanent solution arrives.
Here's how a partnership can work:
-
You secure the new equipment project. Your customer has chosen your team for the long-term solution, and the order is moving forward.
-
A timing challenge comes up. The existing unit fails, production requirements change, or the lead time creates a gap the customer can't comfortably absorb.
-
You explore an interim option with Genemco. We can help you investigate whether a suitable used unit is available for the application.
-
Your customer gets another path to consider. If the equipment is a practical fit, it may help reduce disruption while your team continues delivering the permanent solution.
Not every situation will allow for an interim unit, and used equipment must be evaluated carefully before it is put into service. But when it works, everyone has an opportunity to benefit.
Your customer has another option. Your new equipment project can continue. And you remain the partner helping them navigate the problem.
We respect the relationships OEMs build with their customers. Our goal is to complement your work, not compete with the new equipment solution you've worked hard to sell.
Sometimes, being the hero doesn't mean having a brand-new machine on the floor tomorrow. It means finding a practical way to help your customer get through today while you deliver the right equipment for tomorrow.
Let's Find a Way to Keep Production Moving
Whether you're a plant manager facing an urgent replacement, an engineer evaluating a process upgrade, a maintenance professional searching for a hard-to-find unit, or an OEM trying to help a customer manage a long lead time, you don't have to stop at the first option.
The right solution starts with understanding the application, the operating requirements, and the timeline.
Have a flavorizer, vacuumizer, deaerator, or other food processing equipment need? Explore Genemco's available inventory or contact our team to discuss your requirements.
And if you're an OEM with a customer who needs help in the meantime, let's talk. We're here to help you explore the options, support your customer, and keep the long-term project moving forward.
Because keeping production moving today can make all the difference while the right solution is on its way.


